Smartwatch Back-Cover Appearance Defect Inspection Line
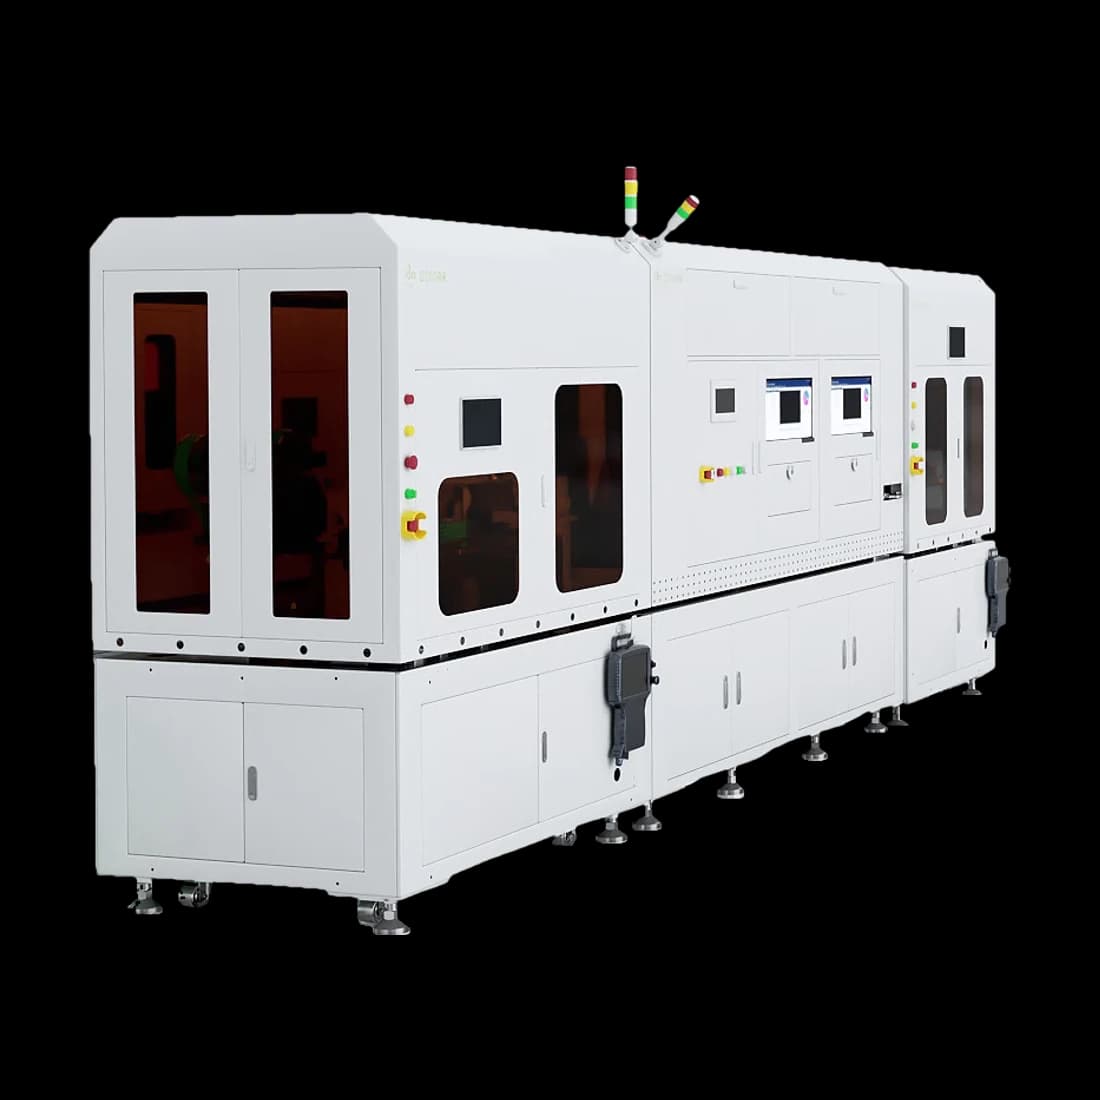
An appearance-defect AOI line for smartwatch back-cover parts, shown in two versions: one for the plastic back-cover frame and one for the assembled back cover. Robots load parts from trays; each part is barcode-read, flipped so that its concave and convex sides are inspected in turn, and unloaded into OK and NG bins. The frame line also removes the protective film and measures the inner slot length and width with two sets of lasers.
- Cycle time (CT)
- 2.5 s/pcs
- Throughput
- 1400+ pcs/H
Specifications
- Overkill rate
- ≤10%
- Escape rate
- 0.5%
- GRR
- ≤10%
- Correlation
- ≤15%
- Suitable products
- Plastic back-cover frames and back-cover assemblies for smartwatches
- Footprint
- 4700(L)*1000(w)*1950(H) mm
- Process
- Robot loading, barcode reading, film removal, flipping (concave side up), concave-side defect inspection, dimension inspection, flipping (convex side up), convex-side defect inspection, robot unloading to OK / NG bins
- Measured dimensions
- Inner slot length and width (two sets of lasers)
- Defect types (back-cover frame)
- Scratches, scuffs, white dots, bright marks, bright spots, particles, burrs, bruises, pressure marks, chipping, over-milling, milling damage, air marks, uneven chamfering
- Defect types (back-cover assembly)
- Scratches, scuffs, bright marks, bright lines, bright spots, shiny areas, white dots, white edges, particles, burrs, bruises, pressure marks, chipping, sand chipping, serration, glue overflow (external, in-slot, internal), dome scratches, dome misalignment, discoloration, oil stains, structural contamination, bubbles, foreign matter, primer
- Loading/unloading method
- Robot loading from trays; robot unloading into OK / NG bins
- Inspection system
- DN software platform (DN Explorer)
See it in action
Silent clips from our 3D machine animations. While a clip is playing, you can pause it from the corner button.
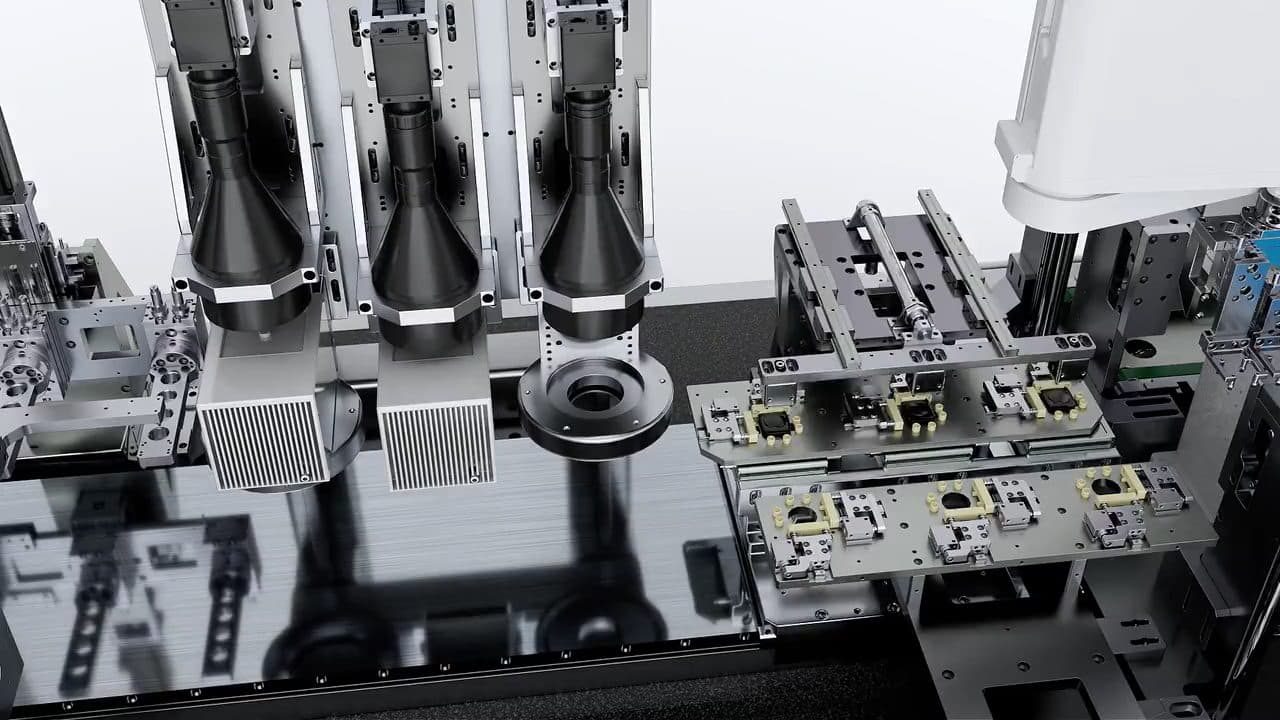
3D animation Inspection station: three camera lenses with their lights on the left, while a robot reaches in to pick parts from the fixture. 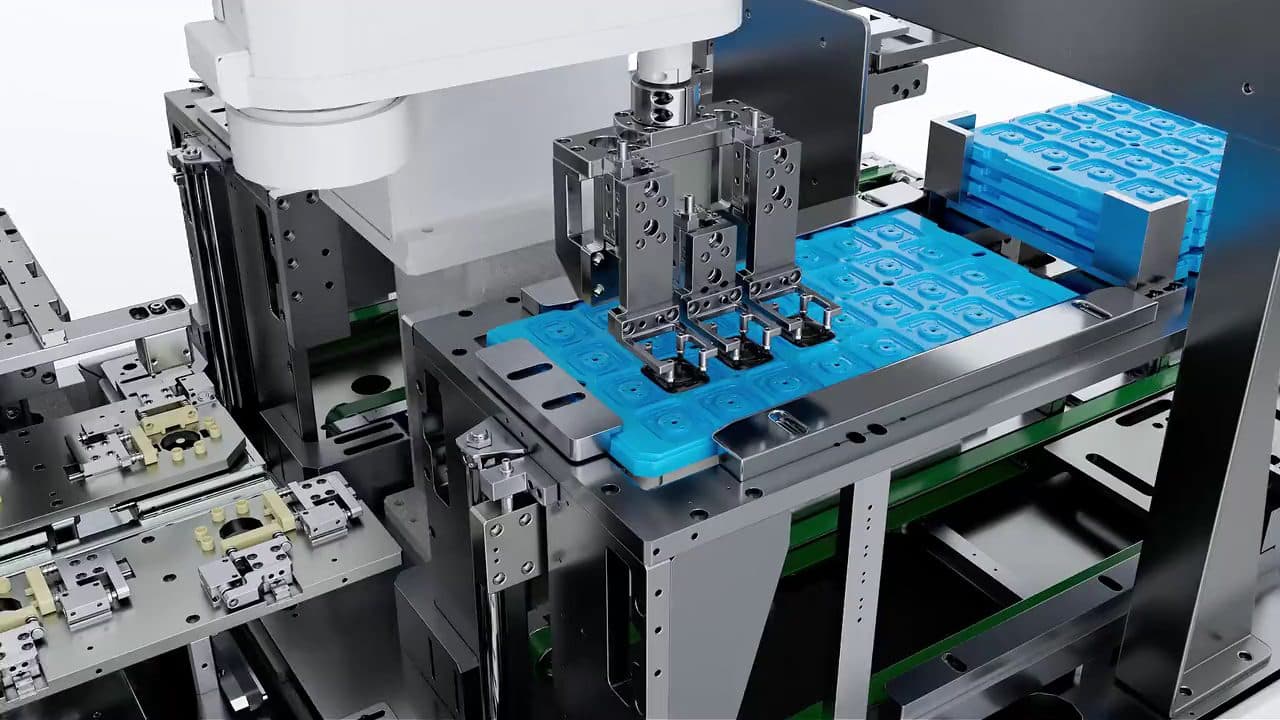
3D animation Unloading: the robot's three grippers set inspected parts into the blue tray row by row until the tray is full.
Highlights

Fast: CT 2.5s/pcs, UPH 1400+pcs/H

Both sides inspected: the part is flipped so the concave side and the convex side each get their own inspection station

Defects and dimensions on one line: two sets of lasers continuously measure the inner slot length and width

Protective film is removed automatically before inspection (frame line)

Robot loading from trays and robot unloading, with OK and NG parts sorted into separate bins

Covers two stages: the back-cover frame (14-item defect list) and the assembled back cover (24-item defect list)
Typical application
Smartwatch back-cover frame and back-cover assembly production lines
Interested in this product?
Contact our engineering team for pricing and technical details.
Talk to an engineer